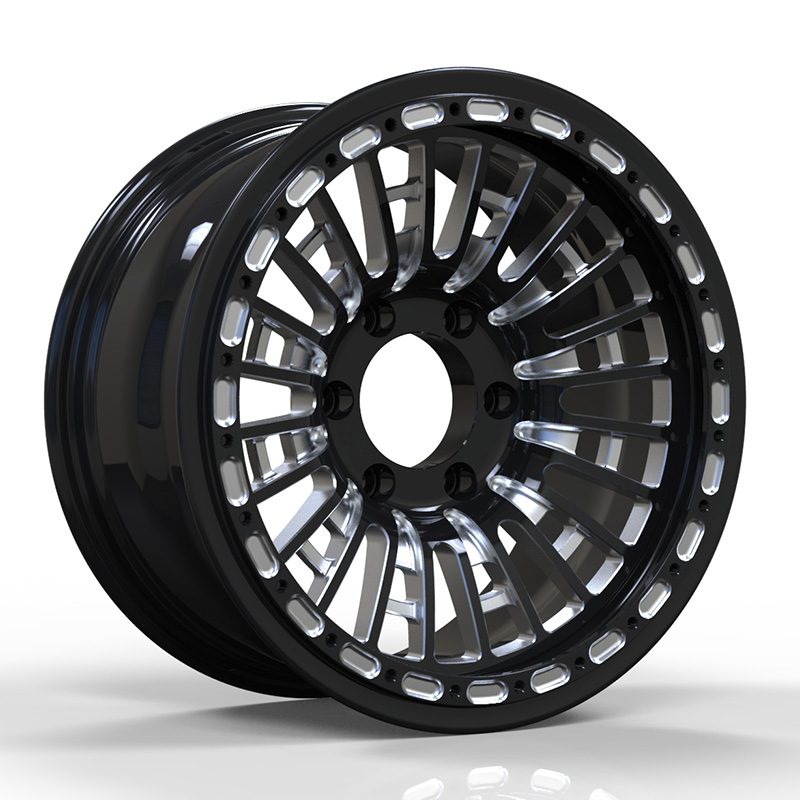
How a forged blank becomes a finished wheel to within a few hundredths of a millimetre, which tolerances actually reach the driver, and where machining errors hide until the first balance check.
CNC machined forged wheels are the point where a forged blank stops being a rough shape and becomes a product with a defined offset, a defined bolt pattern and a defined surface. The forging supplies the material structure; the machining operation decides whether that structure sits in the right place relative to the hub, the brakes and the tyre.
Precision in this context is not an abstract virtue. It shows up as a wheel that runs true at 140 kilometres per hour, that balances with a small correction weight rather than a large one, that tightens flat against the hub without wobble, and that keeps its geometry after a season of thermal cycling. Each of those outcomes traces back to a specific machining decision.
This article follows the machining sequence from datum selection to final inspection, explains which tolerances matter and which are marketing, describes the defects that a buyer can actually detect on receipt, and sets out how a brand should qualify a machining programme before it commits a season of orders to it.
Why the Datum Decides Everything
Every machined wheel is located against a datum, and the choice of datum determines which features are correct with respect to which. Most programmes use the hub mounting face and the centre bore as the primary datum, because those are the surfaces that locate the wheel on the vehicle. Runout measured from anywhere else describes a different part.
A wheel can be geometrically perfect around a badly chosen datum and still vibrate on the car. If the hub face is not flat, the wheel will tighten unevenly and the barrel will tilt by a fraction of a degree, which at the tyre radius becomes a visible lateral movement. That is why hub face flatness is a primary inspection item rather than a secondary one.
The second datum decision concerns the barrel. Machining the bead seats from the hub datum keeps the seats concentric with the mounting face, which is what runout actually measures. Machining them from the outer lip instead can produce a wheel that looks true on a static stand and wobbles once mounted.
For a buyer, the practical implication is that tolerance statements are meaningless without the datum they are referenced to. A supplier who quotes lateral runout without saying it was measured at the bead seat from the hub face has quoted a number, not a specification.
The Machining Sequence for CNC Machined Forged Wheels
The sequence begins with a stress-relieved forged blank and a first operation that establishes the hub face and centre bore. Those two features become the reference for every subsequent cut, so they are produced in a single setup where possible, using a boring operation that keeps them coaxial rather than two separate drilling and facing steps.
Roughing follows, removing the bulk of the material from the spoke windows and the barrel with a large-diameter cutter and a generous allowance for finishing. The roughing strategy matters because it determines how much stress is released and where the part will move. A programme that removes material evenly around the part distorts less than one that cuts one sector to final depth before moving to the next.
Semi-finishing brings the part close to final geometry and gives the finishing pass a consistent allowance to work with. Finishing then produces the surface that the customer sees and that fatigue life depends on: the spoke faces, the window edges, the concave transition and the outer lip. Each of those surfaces has a different requirement, so a single finishing strategy across all of them is usually a compromise.
Drilling and tapping come after the geometry is complete, because hole positions are referenced to the hub face and a hole drilled before final facing will be out of position by the amount of material removed. The bolt pattern is then checked with a position gauge, not with a caliper across two holes, since the gauge describes the pattern and the caliper describes a chord.
| Operation | Feature Produced | Control Point |
|---|---|---|
| First operation | Hub face and centre bore | Flatness and coaxiality, produced in one setup |
| Roughing | Windows and barrel bulk removal | Balanced material removal to limit distortion |
| Semi-finish | Near-final geometry | Uniform allowance for the finishing pass |
| Finishing | Spoke faces, transitions, lip | Surface integrity and dimensional accuracy |
| Bead seat turning | Seats and flanges | Concentricity to the hub datum |
| Drilling and tapping | Bolt pattern and centre cap threads | Position tolerance checked with a gauge |
| Deburring | Window edges and internal corners | Removal without rounding a designed radius |
Tolerances That Reach the Driver
Lateral runout at the bead seat is the tolerance a driver feels first, as a vibration that appears in a narrow speed band and fades above it. Radial runout produces a vertical oscillation that is harder to isolate from tyre variation. Both are measured with a dial gauge on a rotating spindle, and both should be reported in the batch documentation rather than verified only on the first article.
Hub face flatness is the tolerance that decides whether the wheel tightens correctly. A face that is convex will contact at the centre and leave the outer edge free, so the wheel can shift under load even at correct torque. A face that is concave contacts at the rim of the hub and can distort the brake disc hat on a car with a thin mounting flange.
Centre bore tolerance governs how the wheel centres on the hub. A bore that is too small will not seat; one that is too large relies entirely on the lug nuts for centring, which produces a wheel that is technically mounted and practically offset. For vehicles that centre on the bore rather than on the studs, this is a load-bearing tolerance rather than a convenience one.
Offset accuracy is the fourth. A wheel machined to the wrong offset sits in the wrong place relative to the arch, and the error is invisible until the car is on the ground. Offset should be verified by measuring the mounting face position relative to the rim centreline, not by trusting the programmed value in the machine.
Surface Integrity and Residual Stress
A machined surface is not just a shape. Cutting leaves a thin layer with altered residual stress, micro-cracks and a texture that depends on tool geometry, feed rate, cutting speed and coolant. On a wheel spoke, that layer sits exactly where cyclic bending stress is highest, so surface integrity is a fatigue variable rather than a cosmetic one.
A worn tool produces a smeared surface with tensile residual stress and a characteristic dull appearance that does not respond to polishing. Because the visual symptom is subtle, the practical control is tool life management: a defined number of parts or metres of cut per tool, recorded and enforced, rather than a decision made by the operator when the finish starts to look wrong.
Chatter is the second surface defect and the more visible one. It appears as a regular pattern of marks on the spoke face, caused by vibration of the tool or the part during cutting. On a thin spoke the part itself can be the source, which is why support and fixturing design is part of the machining programme rather than an afterthought.
Residual stress from the forging itself is the third factor. A blank that was quenched unevenly carries internal stress that is released as material is removed, causing the part to move between operations. A shop that sees consistent runout drift on a particular design should be looking at the heat treatment and quench, not only at the machining programme.
Machining defects a buyer can detect without a laboratory:
- Regular ripple marks on a spoke face, which indicate chatter during the finishing pass
- A dull patch that will not polish bright, which usually means a worn tool and a stressed surface
- Sharp edges inside a window where the drawing specifies a radius
Deburring, Cleaning and Handling Before Finish
Deburring is the operation that separates a machined part from a finished product. Every cut leaves a burr at the exit edge, and on a wheel those edges sit in the window openings, the bolt holes and the valve bore. A burr left on a window edge is not only unappealing when the wheel is polished, it is a crack initiator under cyclic load and a place where coating builds unevenly.
Hand deburring is still common on complex faces because a tool cannot reach every internal corner without rounding a designed radius. That work is skilled rather than menial: the operator has to remove the burr without changing the geometry, and the difference between a good and a careless job shows up years later as a crack at a window corner or immediately as an inconsistent highlight along a polished edge.
Cleaning follows. Machining coolant, chips and handling marks have to be removed before any coating, because a contaminated surface produces a finish that fails adhesion in the first season. A multi-stage wash with a defined final rinse quality is a production requirement rather than a housekeeping preference, and it is one of the first things to examine on a factory visit.
Handling between machining and finishing is the quiet source of defects. A wheel that is stacked against another wheel, rested on a bare steel trolley or dragged across a bench picks up marks that no polishing will remove without changing the surface. Protective masking, dedicated racks and a no-contact rule for finished faces cost very little and remove a whole category of rework.
It is also worth asking how rejected parts are handled. A shop that reworks a dimensionally out-of-specification wheel by hand and returns it to the batch is introducing variation that the inspection record will not show. A clear scrap rule for anything outside tolerance, applied without exception, is a stronger quality indicator than an impressive list of measuring equipment.
From CAD Model to Machined Part
The transition from a design model to a machining programme is where most schedule problems begin. A model can describe a surface that no cutter can reach, a fillet that no tool can produce, or a wall thickness that cannot be held without deflection. A shop that accepts a model without a manufacturability review discovers those issues at the machine, which is the most expensive place to find them.
A proper review covers tool access to every surface, the minimum internal radius that the largest available cutter can produce, the depth-to-diameter ratio of any pocket, and the fixturing that will hold the part without marking a finished face. Those four items account for most of the redesign work that happens after a first article is cut.
Simulation adds a second layer. Cutting force simulation predicts deflection on thin spokes, and thermal simulation predicts where heat will accumulate during a long finishing pass. Neither replaces a first article, but both shorten the loop between the first and second attempt, which is the part of a programme that customers actually notice.
The output of that process is a documented programme revision rather than a file on a programmer's desktop. A revision number that appears on the inspection record is what allows a factory to answer the question every buyer eventually asks: was this wheel made to the drawing that was approved.
Inspection Equipment and What It Proves
A coordinate measuring machine is the reference instrument for a machined wheel. It reports actual position and form against the model, including features that a gauge cannot describe, such as the true position of a bolt pattern or the profile of a concave surface. A CMM report per design revision is a reasonable expectation for a serious programme.
A runout stand with a dial gauge is the production instrument. It is fast, it measures the feature that matters most to the customer, and it can be used on every wheel rather than on a sample. The value of the stand depends entirely on the fixture: a wheel held on a soft surface will not repeat the measurement to the tolerance being claimed.
A dynamic balancer provides the second production check and reports correction weight in two planes. The size of that correction is a useful proxy for machining quality: a wheel that needs a large weight at one angular position is telling you that material was removed unevenly, even if every dimensional check passed.
Surface inspection closes the set. A visual check under directional light reveals chatter and smearing that a dimensional report cannot, and it is the check that most closely matches what the end customer will see in a showroom. Training an inspector to recognise those patterns is cheaper than discovering them in a container.
Records matter as much as instruments. A measurement that is not written against a serial number cannot be used to investigate a complaint six months later, and a report that lists only pass or fail gives a buyer nothing to compare between batches. The useful format is a short table per wheel showing the measured value, the limit and the instrument used, which turns inspection into a trend rather than a stamp.
Qualifying a Machining Programme Before Volume
The first step is a first-article inspection, not a sample photograph. One wheel from the first batch should be measured fully, documented and retained, and the remaining wheels in that batch should be checked against it rather than against the model. That gives the programme a physical reference that survives staff changes.
The second step is a capability check across a run. Measuring ten consecutive wheels and plotting the runout and balance results shows whether the process is centred or merely passing. A process that produces results just inside a limit on every wheel will fail as soon as anything drifts, and drift is normal in production.
The third step is a change-control agreement. Design revisions, tool changes, new billet suppliers and machine moves all affect the result, and a supplier should notify the buyer before any of them is implemented rather than after the first container ships. That clause costs nothing to write and prevents most of the disputes that arise in a long programme.
- First article retained and measured against the model, with the report tied to a programme revision.
- Ten consecutive parts plotted, so the process is shown to be capable rather than merely compliant.
- Written change control covering design, tooling, billet source and machine relocation.
- A named technical contact who can answer a tolerance question without escalating to sales.
How RETA Controls Machining Quality
RETA has manufactured forged wheels in Ningbo since 2012, with the company founded in 2009, a 12,000 square metre plant and more than 100 staff. Machining, heat treatment and finishing sit inside one facility, which means a tolerance problem can be traced to the operation that caused it rather than negotiated between subcontractors.
The quality system runs on ISO 9001, ISO 14001, ISO 45001 and IATF 16949, with national high-tech enterprise status granted in 2021. Internal limits are held tighter than the SAE, JWL and PCT sequences we design to, and 30-degree and 90-degree impact and deformation tests are added because a machined part's weak points appear at angles a single radial test does not load.
Commercially, the minimum order is one set of four wheels, standard sizes run in roughly 7 to 15 working days and fully custom designs take about 25 to 35 working days. The SSD 1P series is the usual starting point because its machining programmes are already proven, which shortens the distance between a fitment request and a first article.
For buyers who want to compare our approach with general practice in the industry, the note on what makes precision wheel manufacturing different sets out the tolerance philosophy in more detail, and the one piece Y spoke black chrome forged wheel shows how a complex spoke geometry is machined without losing surface quality.
Frequently Asked Questions
Q1. What runout should a CNC machined forged wheel hold?
The figure should be quoted at a defined location, usually the bead seat, measured from the hub datum. A supplier who quotes a runout value without a datum has not given a usable specification, and the number should be verified on every wheel rather than on a first article only.
Q2. Can machining remove a defect that was in the forging?
Only if the defect sits in material that was going to be removed anyway. A subsurface void or a lap that survives into the finished section cannot be machined out without changing the design, which is why incoming billet inspection and forging process control matter more than any downstream check.
Q3. Why does a balanced wheel still vibrate?
Balance corrects mass distribution, not geometry. A wheel with correct balance and excessive lateral runout will still produce a vibration, and so will one with a hub face that is not flat. The two measurements describe different faults and both have to be inside specification.
Q4. Is a five-axis machine enough for a good wheel?
No. The machine provides capability; the programme, the fixturing, the tool management and the inspection decide the result. A well-programmed three-axis operation on a simple design can outperform a poorly supported five-axis cut on a complex one.
Q5. How long does it take to machine a custom wheel design?
A fully custom design typically takes about 25 to 35 working days including programming, a first article and finishing, while a standard size from an existing programme runs in roughly 7 to 15 working days. The difference is almost entirely programming and first-article time.
Send us your model and the tolerances your market requires, and we will confirm how CNC machined forged wheels will be programmed, fixtured and inspected before the first article is cut.
View One-Piece Range Send Drawings